Steel Hub

When technical assessors compare steel wire for real-world use, the right choice rarely comes from the highest tensile value alone. A stronger wire may reduce elongation, complicate forming, shorten fatigue life in dynamic loading, or require a coating that changes cost and corrosion behavior. The practical comparison should start with application load, forming method, service environment, and required service life, then move to tensile strength grades and coating systems that fit those conditions.
This guide explains how to compare steel wire tensile strength and coating options in a specification-driven way. It focuses on what technical evaluation teams usually need most: how to read strength data correctly, how coatings affect durability and processing, and how to avoid selecting a wire that looks strong on paper but performs poorly in production or field service.
What Should Be Compared First: Strength, Coating, or End-Use Conditions?
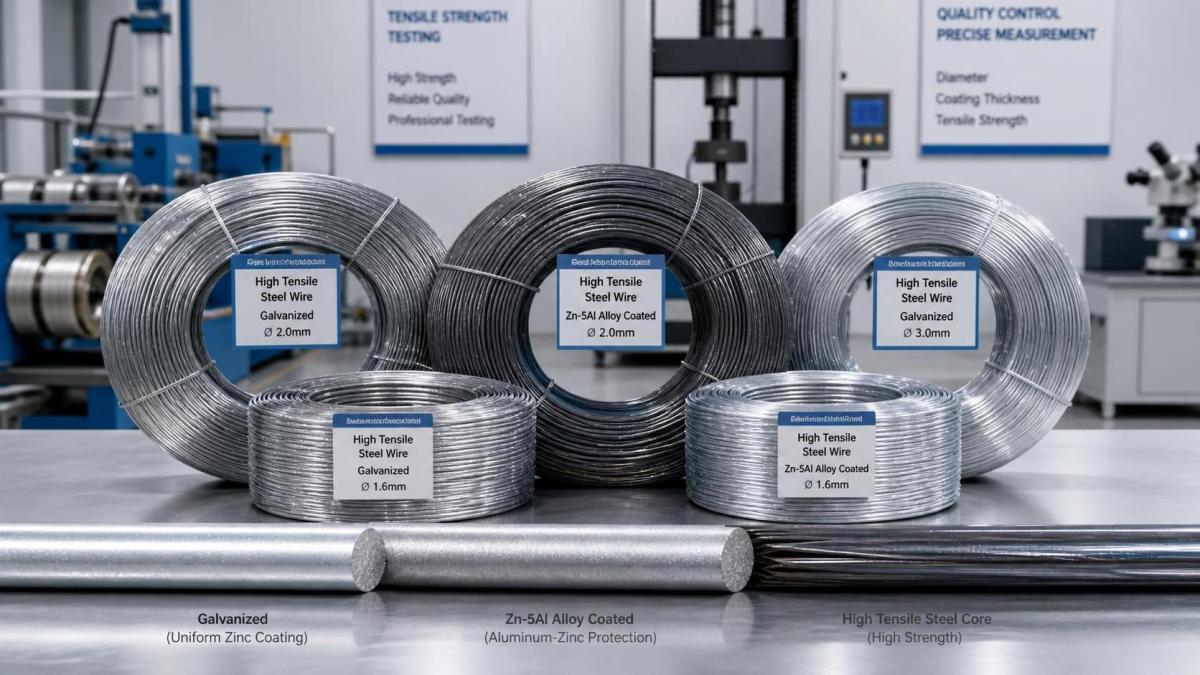
The first comparison should always be the end-use condition, because tensile strength and coating only make sense within a defined application. A wire for springs, prestressed concrete, fencing, fasteners, cable armoring, or cold heading may all require very different balances of strength, ductility, adhesion, and corrosion resistance.
For technical assessors, the most useful starting questions are practical. What static or dynamic load will the wire carry? Will it be bent, twisted, woven, or drawn further? Will it work indoors, in humid outdoor exposure, in marine air, or in contact with chemicals? These answers determine whether high strength, moderate formability, or stronger corrosion protection should lead the decision.
In other words, selection should move from service requirement to material property, not the other way around. This prevents the common error of specifying a very high-strength wire for an application that actually fails because of coating damage, hydrogen-related risk, poor bendability, or shortened life in corrosive conditions.
How to Compare Steel Wire Tensile Strength Correctly
Tensile strength is the maximum stress a wire can withstand before fracture, usually expressed in MPa or N/mm2. In procurement and technical review, this value is often the first item checked, but it should never be interpreted in isolation. A complete comparison must also include yield behavior where relevant, elongation, reduction of area, diameter tolerance, and consistency across production lots.
For many applications, the key question is not simply whether one steel wire is stronger than another, but whether its strength level matches the manufacturing route and service demand. Higher tensile grades can support greater load capacity or allow diameter reduction, but they may also reduce flexibility and increase sensitivity during bending, coiling, straightening, or welding.
Technical assessors should also verify how the reported value was measured. Test method, gauge length, sample preparation, and applicable standard all matter. Comparing a wire tested under one standard against another tested differently can produce misleading conclusions, especially when suppliers present minimum values without showing the full mechanical property range.
Another important point is strength uniformity. For automated manufacturing, variation between coils can be as critical as nominal tensile strength. A wire with slightly lower but tightly controlled strength may produce better forming stability, lower scrap, and more predictable downstream processing than a nominally stronger but inconsistent alternative.
Why Higher Tensile Strength Is Not Always the Better Choice
It is tempting to treat higher tensile strength as an automatic upgrade, but that approach can create hidden production and performance problems. As wire strength increases, formability often decreases. This matters in applications involving repeated bending, crimping, cold forming, or shaping into components that need dimensional stability without cracking.
Fatigue performance is another reason to be careful. In cyclic loading conditions, wire life depends not only on strength but also on surface quality, decarburization control, microstructure, residual stress, and coating integrity. A high-strength wire with surface defects or poor coating adhesion may fail earlier than a lower-strength wire with better surface condition and more balanced processing properties.
Technical assessment should therefore consider the full failure mode. If the dominant risk is overload, a higher strength grade may be justified. If the dominant risk is corrosion-fatigue, abrasion, or bending damage during fabrication, the better answer may be a more moderate strength range with a more suitable surface treatment.
Which Coating Options Matter Most for Steel Wire?
Coating selection is fundamentally about protecting the wire surface while preserving usability in processing and service. The most common options include uncoated bright wire, zinc-coated galvanized wire, zinc-aluminum alloy coatings, polymer-coated systems, phosphate or lubricant carrier coatings for drawing or forming, and specialty plated finishes for specific industrial applications.
Uncoated wire may be acceptable in dry indoor conditions or where the wire will receive a later conversion, plating, or encapsulated assembly. Its advantage is often lower initial cost and cleaner dimensional control, but without added protection it is vulnerable to rust during storage, transport, and service in humid or outdoor environments.
Galvanized steel wire remains one of the most widely used choices because it provides a practical balance between corrosion resistance, availability, and cost. However, technical assessors still need to distinguish between electro-galvanized and hot-dip galvanized products, as coating thickness, durability, surface appearance, and forming behavior can differ substantially.
Zinc-aluminum alloy coatings are often selected when corrosion resistance must exceed standard galvanized performance, especially in aggressive outdoor conditions. Polymer-coated wire can add barrier protection, color coding, or application-specific handling benefits, but it introduces another layer that must be checked for adhesion, abrasion resistance, and compatibility with the installation environment.
How to Compare Coating Performance Beyond Basic Corrosion Claims
Supplier claims such as “excellent corrosion resistance” are not enough for technical evaluation. What matters is measurable coating performance: coating mass or thickness, uniformity, adhesion, expected life in the target environment, resistance to scratching during fabrication, and performance after bending or forming.
For galvanized steel wire, coating mass is a practical starting point because it strongly influences expected service life. Yet more coating is not always automatically better if the wire must undergo severe deformation. A thick coating that cracks or flakes during forming may provide worse real protection than a slightly lighter coating with better adhesion and process stability.
Salt spray test results may be useful as a comparative data point, but they should not be treated as a direct prediction of field life. Outdoor performance also depends on humidity cycles, pollutants, chloride exposure, mechanical wear, drainage conditions, and contact with other materials. Technical assessors should ask for application-relevant evidence, not just laboratory claims.
Coating adhesion deserves special attention in wires that will be bent, woven, twisted, or drawn after coating. A coating that powders, peels, or crazes during conversion can expose fresh steel at the most stressed locations. In many applications, this localized failure controls actual durability far more than nominal coating chemistry.
How Strength and Coating Interact in Manufacturing and Service
Tensile strength and coating should not be evaluated as separate checkboxes. They interact during both manufacturing and use. A stronger wire may require tighter control over surface condition because any notch, crack, or coating defect can become a fracture initiation point. Likewise, some coatings can affect lubricity, friction, weldability, or dimensional consistency in downstream processes.
For example, in cold forming or spring production, the technical team may need a wire with high tensile strength but also very stable surface quality and consistent coating behavior. In fencing or binding applications, slightly lower strength may be acceptable if the wire gains better ductility and a more durable outdoor coating. The correct balance depends on the process window and service risk.
Assessors should also check whether the coating is applied before or after key deformation steps. If substantial forming occurs after coating, adhesion and crack resistance become more important. If the wire is formed first and coated later, then coating coverage, edge protection, and dimensional effects may become the leading concerns.
What Specifications and Supplier Data Should Technical Assessors Request?
A strong evaluation process depends on complete and comparable data. At minimum, request the applicable product standard, steel grade, tensile strength range, diameter tolerance, coating type, coating mass or thickness, test methods, and lot-level quality documentation. Without these details, comparisons between suppliers are often incomplete or distorted.
It is also useful to request elongation, wrap or bend test results, torsion performance where relevant, surface defect criteria, and corrosion test data linked to a recognized standard. For critical applications, ask about heat treatment route, raw material consistency, decarburization control, and process capability for maintaining mechanical stability across repeated orders.
Where supply continuity matters, commercial factors should be reviewed together with technical ones. Lead time, coil size consistency, packaging for corrosion prevention, traceability, and response to claims all affect the total suitability of a steel wire source. A technically acceptable product can still become a poor choice if supply variation disrupts downstream operations.
How to Make a Practical Selection Decision
A practical decision framework is to rank requirements in four layers: load requirement, forming requirement, environmental exposure, and total cost of ownership. Start by defining the minimum mechanical performance needed for safety and function. Next, confirm that the wire can survive fabrication without cracking, flaking, or excessive tool wear.
Then evaluate coating options against the actual service environment instead of generic corrosion labels. Indoor dry use, general outdoor exposure, coastal environments, and chemically aggressive settings should not be grouped together. Finally, compare total cost, including scrap risk, service life, maintenance, replacement frequency, and production efficiency rather than only purchase price per ton.
For technical assessors, this approach usually leads to clearer decisions than a simple two-column strength-versus-price comparison. It also supports better internal communication, because engineering, procurement, and quality teams can see why a certain steel wire grade and coating combination was selected for a specific operating condition.
Common Evaluation Mistakes to Avoid
One frequent mistake is selecting by tensile strength alone and assuming corrosion protection can be handled later. In many cases, surface failure starts long before load capacity becomes the issue. Another mistake is accepting broad coating descriptions without quantified thickness, mass, or adhesion data.
A third mistake is ignoring the effect of downstream processing. Wire that performs well in a tensile test may still fail during coiling, straightening, stamping, weaving, or field installation. Lastly, some teams compare supplier quotations without confirming that all products are built to the same standard and tested with the same method, which can invalidate the entire comparison.
Conclusion: Compare Steel Wire as a System, Not as a Single Number
The best way to compare steel wire tensile strength and coating options is to treat the wire as a system of interacting properties. Tensile strength determines load capability, but coating, surface quality, ductility, processing behavior, and environmental durability often determine whether that capability can be used reliably in practice.
For technical assessors, the most reliable decision comes from matching strength grade and coating type to the real application, then verifying both with comparable data and realistic performance criteria. When the comparison is done this way, material selection becomes more accurate, supply risk drops, and downstream manufacturing or field performance becomes easier to control.
Please give us a message
Tianjin Kaichuang Metal Material Co., Ltd
Add: No. 41, District 6, First Street, Huanghuadian Town, Wuqing District, Tianjin
Tel: + 86 137 9101 9833
E-mail: boss@kaichsteel.com