Steel Hub

If you have ever been in a material review meeting for a new hull or a repair job, you may know the pressure that comes with choosing the right plate. The wrong steel plate for shipbuilding can slow down fabrication, create welding headaches, and leave too many questions around strength once the structure is in service. In practice, the material decision is rarely about one property. It is about how strength, toughness, weldability, plate thickness, and processing conditions fit together.
That is why this choice often becomes a point of confusion. A higher-strength grade may look attractive on paper, but if it is not friendly to welding or forming, it can create more trouble later. On the other hand, a plate that welds easily but does not meet structural demands can also become a weak link. The goal is to avoid both extremes and choose a plate that matches the actual job, not just the specification sheet.
Start with the ship structure, not the grade name
One common mistake is to begin by asking for a familiar grade before defining the real service conditions. A deck plate, a bulkhead, a side shell plate, and a repair patch do not carry the same demands. The first question should be: where will the plate sit, what loads will it see, and how much welding will happen around it?
For shipbuilding, the loading pattern matters as much as nominal strength. Plates in highly loaded regions may need better yield strength and impact resistance, while plates in areas with complex welding may benefit more from stable weldability and predictable fabrication behavior. If the structure has tight fit-up tolerances or many stiffeners, a plate that behaves well during cutting and welding can save time and reduce rework.
It also helps to think about plate thickness early. As thickness increases, welding procedure control becomes more important. Heat input, cooling rate, and restraint all influence the chance of cracking or distortion. A plate that seems suitable in thin sections may require a different evaluation once the thickness changes.
Strength and weldability should be judged together
Strength is usually the first number people look at, but it should not be read in isolation. In shipbuilding, the useful question is not only “how strong is it?” but “can it be welded and fabricated without creating new risks?” That balance is what makes steel plate for shipbuilding different from many general-purpose plate applications.
Weldability depends on several practical factors: chemical composition, carbon equivalent, plate thickness, joint design, and the welding process you plan to use. A plate with higher alloy content may deliver more strength, but it can also increase sensitivity to heat-affected zone issues if the procedure is not adjusted. That does not automatically rule it out; it just means the welding plan and inspection requirements need to be aligned from the start.
In real work, the safer approach is to compare candidate plates against both the design requirements and the fabrication route. If the shop relies on long weld seams, multi-pass welding, or repeated repair welding, the material should be evaluated with those conditions in mind. A plate that performs well under controlled lab assumptions may behave differently on a busy production floor.
Read the material specification the way fabricators actually use it
Specifications are useful, but only if they are read in context. Technical buyers sometimes focus on the minimum strength values and overlook details that affect production, such as delivery condition, plate flatness, allowable thickness tolerance, and whether additional testing is needed for critical parts. These details can affect both fit-up and downstream inspection.
Another point worth checking is whether the plate is intended for normal hull construction, low-temperature service, or a more demanding zone with stricter toughness expectations. The surrounding service environment matters too. Marine exposure, vibration, cyclic loading, and local stress concentration all make surface quality and internal soundness more relevant than they may appear at first glance.
When comparing materials, it is often useful to ask a simple question: if this plate arrives on schedule but needs extra correction before welding, does it still make sense for the job? That question usually exposes whether a material is truly suitable or only technically acceptable.
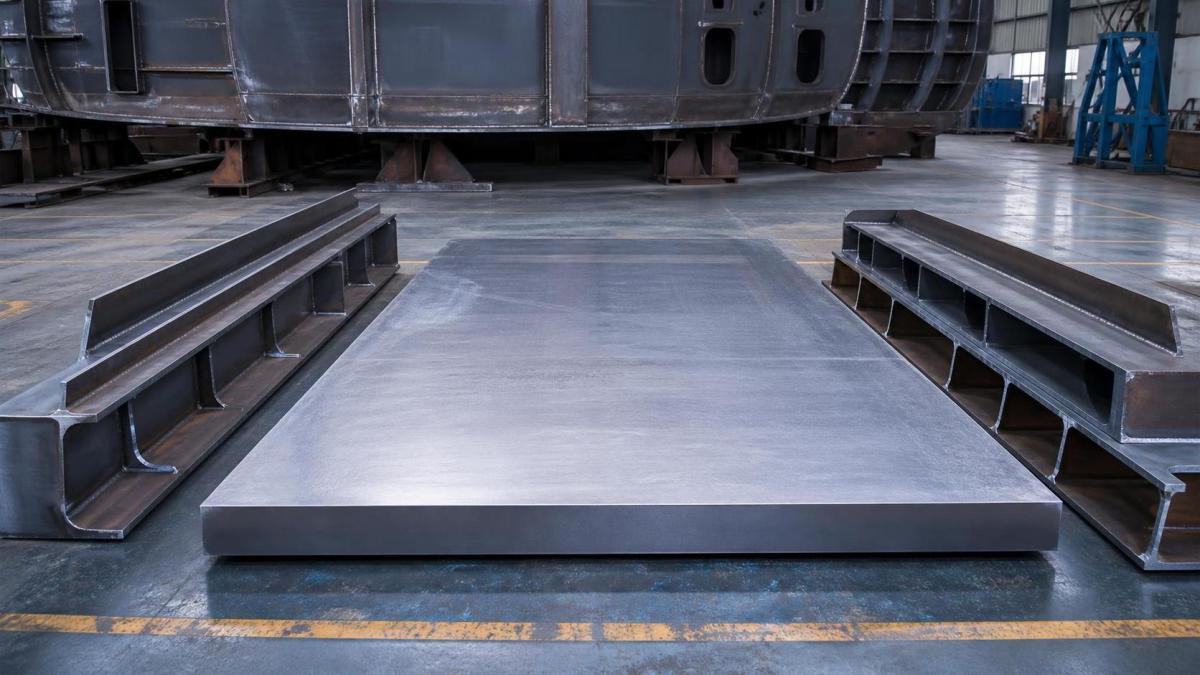
A practical way to compare options
When several plates appear close on paper, a simple comparison routine can keep the decision grounded.
First, check structural demand. Identify whether the plate is carrying primary load, secondary load, or serving mainly as a boundary or support element. This narrows the strength range you actually need.
Next, review weldability indicators. Look at composition limits, expected preheat sensitivity, and whether the planned welding process is compatible with the plate. If the build uses heavy welding or frequent repairs, give extra weight to materials with more stable welding behavior.
Then, confirm fabrication fit. Make sure the plate can handle cutting, bending, and forming without introducing excessive distortion or edge damage. For shipbuilding, poor flatness or difficult forming can create alignment problems long before the ship reaches service.
After that, check inspection needs. Critical structural parts may need closer attention to surface condition, internal integrity, and test documentation. This is not about asking for more paperwork; it is about avoiding surprises during welding or final acceptance.
Finally, compare the whole package rather than one headline value. The right choice is usually the plate that gives enough strength with the least fabrication friction.
Where problems usually show up first
If a steel plate is poorly matched to the job, the first warning signs often appear during cutting and welding, not at sea. Distortion around seams, difficult arc behavior, edge cracking, or repeated repair work can all point to a material-process mismatch. These are the moments when teams realize that selection was based too much on nominal strength and not enough on weldability.
Another common issue is over-specifying the material. Choosing a grade that is stronger than necessary can sound conservative, but it may add welding complexity without improving the structure in a meaningful way. In shipbuilding, “more” is not always “better” if it increases fabrication risk.
That is why many teams benefit from a short review loop before purchase: confirm the intended use, check weld procedure compatibility, and verify that the plate’s mechanical and fabrication characteristics align with the job. This does not require a complicated process, just a disciplined one.
Questions worth asking before release
Before final approval, ask whether the plate grade suits the actual load path, whether the welding procedure can be carried out without special difficulty, and whether the thickness range changes the risk profile. If any of these answers is unclear, it is better to pause and verify than to assume the material will behave as expected.
Also ask whether the plate is being selected for a single structural need or for a broader fabrication sequence. A plate that fits one part of the job but creates bottlenecks in welding or alignment may increase overall cost in ways that are not obvious at quotation stage.
When the decision is still uncertain, bring the review back to a simple rule: pick the steel plate for shipbuilding that satisfies the structural requirement first, then confirm that weldability and fabrication are still comfortable for the shop. That order usually leads to fewer surprises and a smoother build.
In other words, the best choice is rarely the strongest plate on the list or the easiest one to weld in isolation. It is the one that fits the real ship structure, the real welding method, and the real production sequence without forcing unnecessary compromise.
Please give us a message
Tianjin Kaichuang Metal Material Co., Ltd
Add: No. 41, District 6, First Street, Huanghuadian Town, Wuqing District, Tianjin
Tel: + 86 137 9101 9833
E-mail: boss@kaichsteel.com