Steel Hub

Knowing whether a carbon steel pipe meets ASTM standards is not a paperwork exercise. For technical evaluators, it is a practical decision about whether the pipe can be trusted in service, whether the supplied material matches the design basis, and whether downstream fabrication or installation risks are being introduced before the first cut, weld, or pressure test.
That judgment is rarely made from one document alone. A pipe may carry an ASTM designation in a quotation, on a stencil, or even on a mill test report, yet still fall short in dimensions, chemistry, heat treatment condition, mechanical properties, or traceability. The real task is to confirm that the supplied pipe conforms to the specific ASTM specification claimed for it, not just that it is “ASTM-like” or generally suitable carbon steel.
In practice, the question should be framed more precisely: which ASTM standard, for what product form, for what service condition, and with what mandatory supplementary requirements? Carbon steel pipe is covered by multiple ASTM specifications, and compliance can only be assessed against the exact one referenced by the project, purchase order, code, or customer standard.
Start with the exact ASTM specification, not the generic label
One of the most common evaluation errors is treating “ASTM pipe” as a single quality category. It is not. ASTM standards for carbon steel pipe differ by manufacturing route, intended service, testing scope, and acceptance criteria.
Examples commonly seen in industrial procurement include ASTM A53, ASTM A106, ASTM A333, ASTM A671, ASTM A672, and ASTM A691, among others. Even within a single specification, grade and type matter. A53 Grade B is not interchangeable with A106 Grade B simply because both are carbon steel pipe and both are frequently used in pressure-related applications. Their manufacturing allowances, required tests, and intended application contexts differ.
Before reviewing the pipe itself, confirm four basic references:
- the ASTM specification number and edition referenced by the order or project documents;
- the material grade;
- the pipe form and manufacturing method, such as seamless, ERW, or SAW;
- any supplementary requirements from ASME, project specifications, end-user standards, or third-party inspection plans.
If any of these are unclear, technical verification becomes unreliable. A pipe can fully comply with one ASTM specification and still be non-compliant for the intended project because the wrong standard was ordered in the first place.
Check the marking, but do not stop there
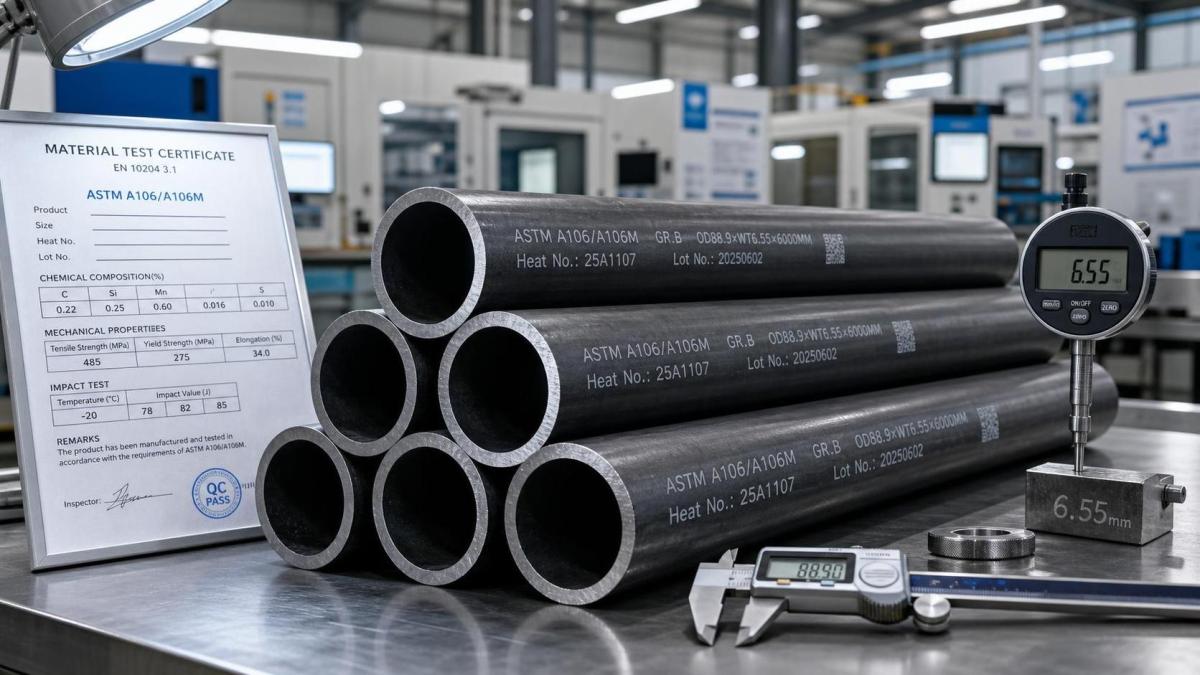
Pipe marking is the fastest first screen. ASTM-compliant carbon steel pipe is typically marked with at least the manufacturer’s name or trademark, specification, grade, size, schedule or wall thickness where applicable, heat number or traceability code, and sometimes manufacturing process.
Marking helps answer two early questions:
- Does the physical pipe correspond to the material described in the documents?
- Can the pipe be traced back to a specific heat, lot, or production batch?
If the stencil is incomplete, inconsistent, or not traceable to the mill test report, the risk increases immediately. That does not automatically prove non-compliance, especially if markings were damaged in logistics or coating operations, but it does weaken verification. For technical evaluators, traceability is often as important as nominal conformity, particularly for pressure service, regulated sectors, or projects requiring full material control.
A useful rule in inspection practice is this: marking supports compliance, but marking alone does not establish compliance.
Review the mill test report as a technical document, not a formality
The mill test report, often called MTR or EN 10204-type certification depending on documentation practice, is usually the core record used to verify ASTM compliance. The problem is that many reviews remain superficial: the evaluator checks the grade, sees a stamp, and moves on. That is where avoidable failures begin.
When reviewing an MTR for a carbon steel pipe, focus on whether it demonstrates conformance to the specific ASTM standard claimed. Key points usually include:
- manufacturer identity and production facility;
- ASTM specification and grade;
- heat number and product traceability;
- chemical composition results;
- mechanical test results;
- dimensions and mass data where applicable;
- required nondestructive or hydrostatic test records;
- heat treatment condition if required by the standard;
- signature or authorization by the responsible quality function.
The critical step is not just reading the reported values, but comparing them against the limits stated in the relevant ASTM specification. A report that lists chemistry and tensile results is not enough if those values fall outside the allowed range, if mandatory tests are missing, or if the test frequency does not meet the standard.
Another point worth watching is the use of copied or reformatted certificates from traders rather than original mill-origin records. Reissued documents are common in international trade, but they should still preserve original traceability and test data. If the chain from mill to supplied pipe cannot be demonstrated, compliance confidence drops sharply.
Chemical composition must match the grade, not just “carbon steel”
Technical evaluators often encounter a misleading assumption: if the material is carbon steel and the tensile strength is acceptable, chemistry is a secondary issue. In ASTM pipe evaluation, chemistry is foundational because it affects weldability, strength response, low-temperature performance, heat treatment behavior, and code acceptability.
The exact chemical limits depend on the ASTM specification and grade. Carbon, manganese, phosphorus, sulfur, silicon, and sometimes additional elements may be controlled. The evaluator should check the reported ladle or product analysis against the standard requirements and pay attention to the following:
- whether all required elements are reported;
- whether maximum limits for residual or detrimental elements are respected;
- whether the chemistry is consistent with the claimed manufacturing route and grade;
- whether any deviation could affect welding procedure qualification or service suitability.
For example, excessive carbon equivalent may not disqualify a pipe under every ASTM clause by itself, but it can create fabrication and weld integrity concerns. So even when the MTR appears formally acceptable, chemistry should be assessed in the context of the actual use case.
Dimensions and tolerances are part of ASTM compliance
Many disputes arise because a supplied pipe has acceptable chemistry and strength but fails dimensional checks. ASTM compliance is not limited to material properties. Outside diameter, wall thickness, length, straightness, end condition, and weight tolerance may all be covered by the applicable specification.
This matters more than it sometimes appears on paper. Wall thickness variation affects pressure design margin. Ovality can complicate fit-up and welding. Excessive under-thickness at a local point can trigger rejection even if average thickness looks acceptable. End squareness and bevel quality can also affect field productivity and weld quality, especially on large projects.
Technical evaluation should therefore include physical measurement, not only document review. At minimum, confirm:
- outside diameter against nominal size tolerance;
- wall thickness at multiple locations;
- length and length tolerance;
- pipe end finish and bevel where required;
- surface condition, including seams, laminations, dents, scabs, and gouges.
If the pipe is coated, lined, or bundled on arrival, dimensional verification may need to be built into incoming inspection procedures before the material becomes difficult to access.
Mechanical properties should be evaluated in context
Tensile strength, yield strength, and elongation are frequently the headline numbers on a certificate, but their interpretation requires care. ASTM standards define both the required values and the corresponding test methods or acceptance basis. Technical evaluators should verify that the reported results satisfy the applicable minimums and that the test specimen orientation, sampling location, and test frequency align with the standard.
Be cautious when values look unusually high. Higher strength is not automatically better. Very high reported tensile or yield values can suggest chemistry drift, excessive work hardening, or mismatch with the expected metallurgical condition. In some fabrication environments, that can reduce formability or complicate welding performance.
For services involving low temperature, impact testing may also become essential, but the requirement depends on the specification and project basis. ASTM A333, for instance, is specifically associated with low-temperature service, whereas standards such as ASTM A53 or A106 are not automatically substitutes simply because the basic strength seems comparable.
Manufacturing method and heat treatment are often decisive
A carbon steel pipe can look identical externally while differing significantly in how it was produced. ASTM standards may distinguish between seamless and welded pipe, and in welded products the weld seam manufacturing method can matter. Some standards also require normalization, normalizing and tempering, or other heat treatment conditions for certain grades or classes.
This is not a procedural detail. Manufacturing route influences internal soundness, dimensional consistency, toughness behavior, and inspection requirements. If a specification requires seamless pipe, a welded pipe cannot be accepted as equivalent without explicit engineering and code approval. If post-weld heat treatment is mandatory for a class of pipe, missing that step may invalidate the material for the intended service.
Technical evaluators should therefore verify that the MTR, production records, and pipe marking consistently state:
- the manufacturing process;
- the weld condition where relevant;
- the heat treatment performed;
- the test regime associated with that production route.
Required testing is where weak compliance claims often fail
ASTM pipe standards usually specify one or more required tests beyond chemistry and tensile properties. Depending on the specification, these may include hydrostatic testing, nondestructive electric testing, flattening tests, bend tests, impact tests, and visual or dimensional examination.
This is one of the most common weak points in trade documentation. A supplier may declare compliance to an ASTM standard but provide test data only for chemistry and tensile results. If the standard also requires hydrostatic or NDE examination, and there is no evidence it was performed, compliance is not fully demonstrated.
Look closely at whether the standard permits one test as an alternative to another. Some specifications allow hydrostatic test or nondestructive electric test under defined conditions. Others have more specific requirements. The evaluator should not assume interchangeability without checking the actual ASTM text or approved purchasing specification.
Where service criticality is high, third-party witness or review may be justified even when documentary evidence is available. This is especially true for export orders crossing multiple intermediaries, where document integrity and physical lot integrity are not always equally strong.
Surface quality and workmanship should not be treated as cosmetic issues
ASTM acceptance also involves workmanship criteria. Surface defects, weld seam irregularities, laminations, arc strikes, handling damage, and repair marks can all affect acceptability depending on severity and standard provisions. Some discontinuities may be removable within wall tolerance; others are rejectable.
For technical evaluators, the practical question is whether the observed condition remains within allowable limits and whether remedial grinding or repair has been controlled and documented. If pipes have already been coated, defects can be concealed. That makes pre-coating inspection more valuable than post-delivery argument.
Be careful with substitutions, mixed lots, and “equivalent” claims
In international sourcing, substitutions are often presented as commercially reasonable. A supplier may suggest that one carbon steel pipe grade is “better than” the specified grade, or that one ASTM standard is “equivalent” to another. Sometimes there is partial overlap in chemistry or strength, but that does not create automatic compliance.
Three risks appear repeatedly:
- mixed heats or mixed standards in the same shipment;
- pipe supplied to a neighboring but not identical specification;
- documents showing one standard while physical marking or dimensions suggest another.
For technical evaluators, any substitution should be handled as an engineering deviation, not an informal upgrade. Acceptance should depend on design code requirements, service conditions, welding implications, inspection scope, and customer approval.
A practical verification sequence for incoming evaluation
When time is limited, a disciplined sequence helps separate acceptable material from questionable lots quickly:
- Confirm the exact ASTM specification, grade, edition, and any supplementary project requirements.
- Match pipe marking to the purchase order and MTR traceability data.
- Review chemical composition against the stated ASTM limits.
- Review mechanical properties and check test frequency and method basis.
- Verify manufacturing route, heat treatment condition, and required tests.
- Measure critical dimensions and inspect surface condition on sampled pieces or the full lot as required.
- Resolve any inconsistencies before release to fabrication or installation.
This approach is especially important where the cost of late rejection is high. Once pipe is cut, welded, machined, painted, or installed, a basic standards verification issue becomes a project claim, not a simple receiving inspection problem.
What actually proves ASTM compliance
A carbon steel pipe should be considered ASTM-compliant only when the full body of evidence lines up: the correct specification has been ordered, the marking is traceable, the mill documentation is credible, the chemical and mechanical results meet the standard, the dimensions and workmanship are within tolerance, and all required tests and production conditions have been satisfied.
That may sound strict, but in technical evaluation it is the difference between formal compliance and assumption. ASTM standards are not brand labels. They are detailed requirements, and the only reliable way to verify them is to test the claim against the exact standard and the actual delivered pipe.
For organizations sourcing across borders or through trading channels, that discipline has another benefit: it reduces not only quality risk, but also disputes over liability, code acceptance, and downstream performance. In steel procurement, the cheapest mistake is the one caught before the pipe reaches production.
Please give us a message
Tianjin Kaichuang Metal Material Co., Ltd
Add: No. 41, District 6, First Street, Huanghuadian Town, Wuqing District, Tianjin
Tel: + 86 137 9101 9833
E-mail: boss@kaichsteel.com