Steel Hub

Start with the approval basis, not the factory tour
Quality control at a carbon steel pipe manufacturer can only be verified against a defined acceptance basis. A clean workshop, modern equipment, or a long list of certificates may indicate a capable supplier, but none of them proves that a specific pipe order will meet the service requirements.
Before reviewing the manufacturer, the buyer's quality or safety team should establish four items: the applicable product standard, the pipe grade and delivery condition, the intended service, and the inspection documents required for release. These points determine what must be controlled. Pipe for structural fabrication, low-pressure water conveyance, fire protection, boiler service, pressure piping, or sour environments may all be described as carbon steel pipe, yet their failure modes and acceptance criteria differ substantially.
A useful audit question is: can the manufacturer show how its inspection plan changes when the standard, grade, size range, or end use changes? If the answer is limited to a generic quality manual, the site may have a formal system without sufficient product-level control.
For each order, the supplier should be able to identify the governing specification, revision, supplementary requirements, heat treatment condition where applicable, test frequency, acceptance limits, marking rules, and required certification level. Those requirements should appear consistently in the purchase order review, production traveler, inspection records, and final material certificate.
Traceability must survive every production step
Traceability is the foundation of pipe quality verification because many important properties cannot be judged from the finished surface. A pipe may look dimensionally correct while having the wrong chemistry, insufficient toughness, an unqualified weld seam, or a test record belonging to another production lot.
Begin at incoming material control. For seamless pipe, this usually means verifying the identity and certification of billets or blooms. For welded pipe, the audit should cover coil, strip, or plate receipt and the control of incoming material condition. The manufacturer should have a defined process for checking supplier certificates, material grade, heat number, dimensions, surface condition, and segregation status before material enters production.
The most important point is not whether a heat number exists on paper. It is whether that identity remains connected to the pipe after cutting, forming, welding, sizing, heat treatment, finishing, bundling, and shipment. This connection can be maintained through physical marking, barcode systems, route cards, controlled batches, or another documented method. The method may vary, but it must prevent mixing and permit backward investigation.
Ask the manufacturer to select a finished bundle at random and trace it back to the original raw material heat. Then reverse the exercise: select an incoming heat and ask which finished pipes were made from it. A system that works only in one direction may not support an effective recall or failure investigation.
Particular attention is needed when production involves multiple heats, short-length orders, rework, or cut-to-length operations. These are common points at which identification can be lost. If pipes are transferred between workstations without controlled labels or electronic records, the risk of certificate-to-product mismatch rises sharply.
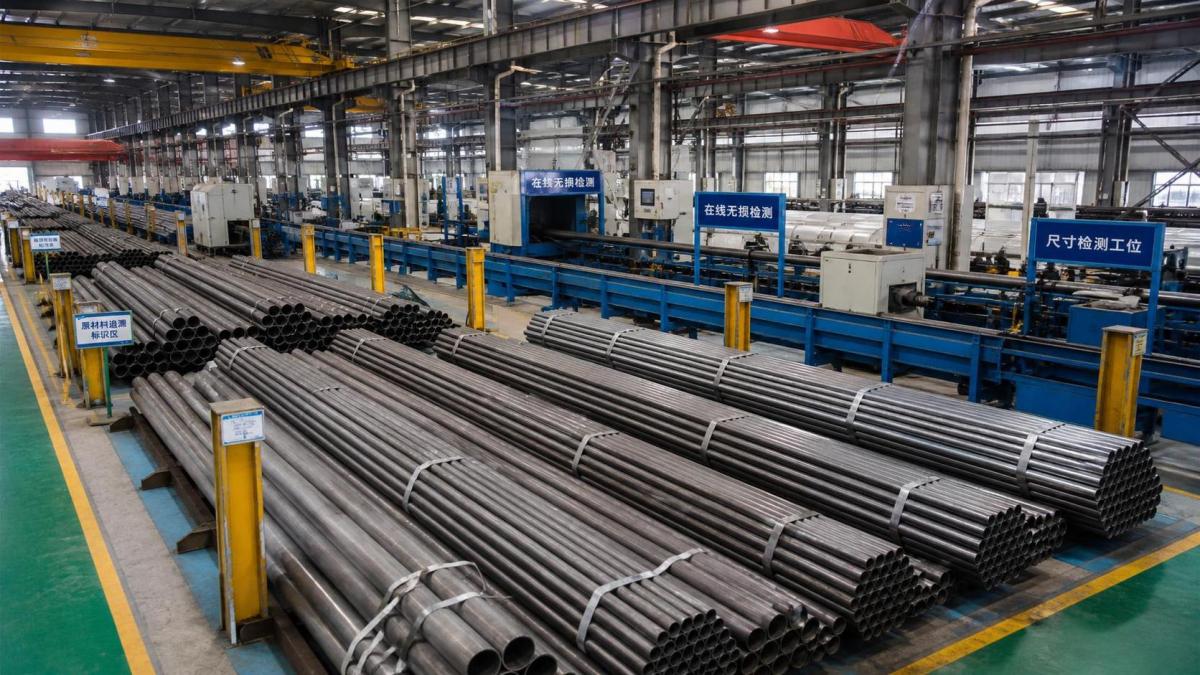
Chemical composition control should be tied to the actual grade
Mill certificates are necessary, but they should not be treated as the whole chemical-control process. A capable manufacturer defines how it verifies incoming chemistry, how it handles material outside the permitted range, and when it conducts check analysis on production material.
The required elements depend on the specified standard and intended use. Carbon, manganese, phosphorus, sulfur, silicon, and residual elements may affect weldability, strength, ductility, corrosion performance, and suitability for subsequent fabrication. For pipes expected to be welded in the field or fabricated into pressure-containing assemblies, composition limits can have practical consequences beyond the minimum mechanical properties shown on a certificate.
Quality teams should confirm that the test method is appropriate for the material form and that the laboratory equipment is controlled. Optical emission spectrometry is commonly used for rapid alloy verification, while combustion methods may be used where accurate carbon or sulfur determination is needed. The audit should cover calibration, reference materials, operator authorization, sample preparation, and the action taken when a result is close to or outside a limit.
A frequent weakness is relying on a single certificate value while ignoring heat segregation. If several heats are processed in the same production campaign, the manufacturer must preserve the identity of each heat or use a documented lot-control approach permitted by the relevant standard. “Same grade” does not automatically mean “interchangeable for certification.”
Review process controls where pipe defects are created
Inspection at the end of the line cannot fully compensate for unstable manufacturing controls. The audit should focus on the stages at which defects can originate, especially for the pipe type being supplied.
For welded carbon steel pipe
Welded pipe quality depends heavily on strip preparation, forming stability, welding parameters, weld seam treatment, and online inspection. The supplier should be able to demonstrate control of edge condition, strip alignment, welding current or energy input, welding speed, squeeze force where relevant, and seam heat treatment when specified.
For electric resistance welded pipe, ask how the manufacturer verifies weld integrity and detects common discontinuities such as lack of bonding, penetrators, hook cracks, cold welds, or seam inclusions. The appropriate inspection method depends on the product standard and application, but the manufacturer should have defined equipment settings, verification standards, alarm response procedures, and records showing that the inspection system was functioning during production.
Weld repair needs close scrutiny. Some specifications prohibit repair welding; others permit limited repair under controlled conditions. A manufacturer should not make this decision informally on the shop floor. The procedure must state whether repair is allowed, who authorizes it, how the repaired area is examined, and how the pipe remains identifiable after repair.
For seamless carbon steel pipe
Seamless pipe removes the longitudinal weld seam but introduces other control points. Piercing, elongation, rolling, reheating, sizing, straightening, and heat treatment can affect wall thickness, eccentricity, surface quality, grain structure, and mechanical properties.
During an audit, examine how the producer controls billet quality before piercing and how it identifies internal or external defects that may become more severe during deformation. The manufacturer should also be able to explain its control of temperature windows, tooling condition, reduction schedule, and straightening practices. Excessive straightening can mask shape problems while creating surface damage or local stress.
Heat treatment requires more than recording furnace temperature. The supplier should define loading practice, soaking time, temperature uniformity, cooling method, lot identification, and response to furnace deviations. Where mechanical properties depend on normalizing, normalizing and tempering, quenching and tempering, or another delivery condition, the heat-treatment record is part of the evidence that the pipe conforms.
Dimensional checks should reflect installation and service risk
Outside diameter, wall thickness, length, straightness, ovality, end preparation, and mass are not simply catalog values. They affect fit-up, welding, pressure capacity, threading, bending, coating, and the ability to assemble the pipe into a larger system.
Verify both the measurement method and the sampling plan. A supplier may have gauges available but use them inconsistently, measure only convenient locations, or sample at a frequency that does not detect process drift. The audit should establish where dimensions are measured, how often readings are taken, how gauges are calibrated, and what happens when a dimension approaches a tolerance boundary.
- Wall thickness should be checked at locations that can reveal eccentricity, not only at a single accessible point.
- Outside diameter and ovality should be assessed after relevant forming, sizing, heat treatment, and straightening operations.
- Pipe end condition should be reviewed where the product will be beveled, threaded, grooved, expanded, or joined by automated welding.
- Length control should account for trim loss and allowable tolerance, especially where pipes are supplied for prefabricated spools or structural assemblies.
Do not accept a general statement that all dimensions are checked “according to standard” without identifying the specific standard and product range. Tolerances can differ by manufacturing route, nominal size, wall designation, end type, and ordered condition.
Mechanical, pressure, and non-destructive testing need a clear sampling logic
Mechanical testing confirms that the production route delivered the required material properties. Typical tests may include tensile testing, flattening, bend testing, flaring, flange testing, impact testing, or hardness testing, depending on the applicable standard and application. The correct question is not whether the manufacturer performs every possible test. It is whether the required tests are conducted on representative samples at the prescribed frequency and under controlled conditions.
Review how the test lot is defined. A test sample taken from one pipe cannot automatically represent every pipe in a large production run. The manufacturer should be able to show the relationship among heat, size, wall thickness, heat-treatment batch, production lot, and test specimen. If the standard permits grouping, the grouping rules should be documented rather than assumed.
Hydrostatic testing deserves special attention for pressure-related service. The test verifies the pipe's ability to withstand a specified internal pressure for a stated period or under a defined procedure. It does not guarantee unlimited service life, nor does it replace correct design, joining, corrosion control, and installation. However, missing, bypassed, or poorly recorded hydrostatic testing is a serious release concern when the specification requires it.
During a site assessment, inspect whether test pressure is automatically recorded, whether gauges or transducers are calibrated, whether hold time is controlled, and how failed pipes are segregated. A hydrostatic tester that passes every pipe without a documented challenge or verification routine provides limited assurance.
Non-destructive examination must be evaluated in the same way. Ultrasonic, eddy-current, magnetic particle, radiographic, or other methods may be required depending on the product and standard. Verify the procedure qualification, operator competency, reference standards, equipment checks, sensitivity settings, reject handling, and record retention. An NDT report has value only when the inspection method was capable of detecting the discontinuities that matter for the ordered product.
Documentation review is where control-system gaps become visible
The final document package should allow a purchaser to connect the delivered pipes to the required standard, material heat, manufacturing route, testing, inspection disposition, and shipment identity. A typical review may include material test certificates, inspection reports, dimensional records, hydrostatic or NDT records where required, heat-treatment charts, calibration status for critical instruments, and nonconformance records relevant to the supplied lot.
Look for consistency rather than volume. Conflicting heat numbers, impossible test dates, incomplete lot references, altered fields, or certificates that do not identify the delivery condition can reveal weak process discipline. A certificate that lists compliant chemistry and tensile values is insufficient if it cannot be matched to the pipe markings and bundle numbers delivered to site.
Document control should also include change management. A manufacturer may substitute raw material sources, move production to another line, alter a welding process, change a heat-treatment cycle, or use a different inspection method. When such a change affects an approved product, the supplier needs a defined review and notification process. This is particularly important for safety-sensitive applications where qualification was based on a specific route or facility.
Use nonconformance handling to judge the supplier's maturity
Every manufacturing operation produces occasional deviations. The useful distinction is between a supplier that detects, contains, investigates, and prevents recurrence, and one that simply removes the affected item without understanding the cause.
Ask to review anonymized examples of recent nonconformance reports. The records should show how suspect material was identified, quarantined, evaluated, dispositioned, and released or rejected. They should also show whether the root cause was examined and whether corrective actions were verified. A quality system that records only “reworked” or “accepted by inspection” without explaining the basis may allow the same problem to return.
Pay close attention to concessions. Any departure from the order requirement should be visible to the purchaser and formally accepted where the contract requires it. Uncommunicated substitution of test frequency, material source, wall thickness range, or repair practice can create compliance and liability issues even when the pipe appears usable.
Approve the manufacturer only after verifying repeatability
A single successful sample or one well-prepared audit day should not be the final basis for approval. The objective is to determine whether the manufacturer can repeatedly produce traceable, conforming carbon steel pipe across the size range, grade, and production route relevant to the order.
For critical applications, approval is stronger when the review combines a document audit, a shop-floor walk-through, traceability challenge, observation of critical tests, and inspection of a recent production lot. The findings should be translated into practical controls: defined hold points, required certificates, independent witnessing where justified, pre-shipment document review, and a clear escalation path for nonconformities.
A manufacturer with fewer marketing claims but disciplined lot control, calibrated inspection, coherent records, and transparent deviation handling is usually easier to manage than one that offers broad capability without evidence connecting its controls to the pipe being shipped.
Please give us a message
Tianjin Kaichuang Metal Material Co., Ltd
Add: No. 41, District 6, First Street, Huanghuadian Town, Wuqing District, Tianjin
Tel: + 86 137 9101 9833
E-mail: boss@kaichsteel.com