Steel Hub

Wall thickness for a pressurized stainless steel pipe should be selected from the service conditions first, not from a preferred schedule or a past project shortcut. The starting point is the design pressure and design temperature, then the outside diameter, material grade, allowable stress from the governing code, corrosion allowance, manufacturing tolerance, and any extra loads that the line will see after installation. A pipe that looks adequate on a simple pressure basis can still be too thin once corrosion, thread cutting, cyclic loading, field handling damage, or support spacing are considered.
For most pressure service, the practical question is whether the chosen wall still has enough remaining thickness after every deduction that matters. That means the nominal wall is only the first number in the conversation. The more useful number is the minimum required wall at the most severe design condition, plus any added allowance that the system actually needs in operation.
Start with the governing design condition
A line may operate at one pressure and one temperature most of the time, yet need to be sized for another condition entirely. Pressure testing, upset conditions, pump deadhead, thermal expansion during blocked-in service, steam-out, or cleaning cycles can control the requirement. If the specification only reflects normal operation, the selected wall may be thin on paper before the pipe is even purchased.
Temperature matters because allowable stress for stainless steel generally changes with temperature, and that directly affects the required thickness under the code formula being used. The difference can be significant enough that a pipe schedule acceptable at ambient temperature no longer provides margin at elevated temperature. For low-temperature service, toughness and weld procedure suitability also need attention, even when pressure thickness itself looks modest.
Do not treat nominal size and actual wall as the same thing
One common source of error is mixing nominal pipe size, outside diameter, and wall thickness from different standards. Pipe schedules are standardized, but the actual wall behind Schedule 10S, 40S, or 80S must be verified against the specific size being used. A thin-wall large-diameter line may become vulnerable much faster than a smaller line under the same pressure because hoop stress rises with diameter.
That is why wall thickness choice should be made using the actual outside diameter and the code equation, then compared with available schedule thicknesses. Selecting a familiar schedule first and confirming later often leads to repeated redesign, especially where reducers, branch connections, and mixed end preparations are involved.
Corrosion allowance is not automatic for stainless steel
Many stainless grades are chosen because the corrosion rate is expected to be low, but that does not mean corrosion allowance can be ignored by default. The need depends on the medium, chlorides, acidity, cleaning chemicals, solids carryover, erosion zones, and whether the pipe will be exposed internally, externally, or both. In some services, general corrosion may be limited while pitting, crevice attack, or stress corrosion cracking becomes the real threat. Those damage mechanisms are not solved simply by adding wall, but thickness still affects inspection interval, remaining life, and tolerance to local metal loss.
If the process fluid is clean and the grade selection is well established, the allowance may be minimal or even omitted under the project rules. If the service is uncertain, intermittently wet, contaminated by chlorides, or subject to washdown chemicals, assuming zero allowance can create a narrow operating window. External conditions matter as well: insulation traps moisture, marine atmospheres deposit salts, and support contact points can become localized corrosion sites.
Manufacturing tolerance can consume part of your margin
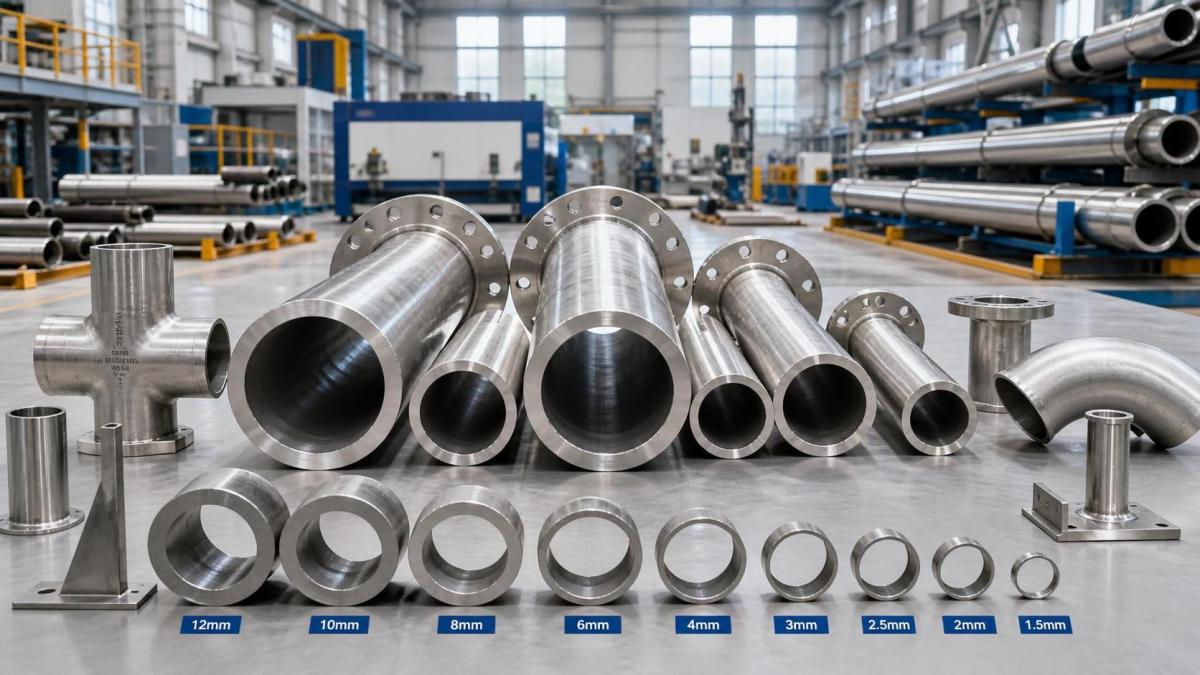
Specified wall thickness is not the same as guaranteed thickness at every point on the pipe. Product standards may permit a negative wall tolerance, and that tolerance has to be considered when comparing a nominal schedule to the calculated minimum. If the engineering calculation says the line needs a thickness close to the lower manufacturing limit of a given schedule, the selection is already too tight. This is especially relevant on thinner schedules, where a small absolute variation can represent a large percentage of the wall.
Field experience also supports leaving room beyond the bare minimum. Minor ovality, handling marks, bevel preparation, and local grinding around fit-up can all reduce effective thickness in limited areas. None of these conditions should drive major oversizing, but they are enough to justify avoiding a knife-edge decision between two schedules.
Welding details can change the thickness decision
A straight run may pass the pressure calculation, while fittings and branch connections become the weak points. Reinforcement requirements around nozzles, stub-ins, sockolets, or weldolets are influenced by the available wall in the run pipe. Thicker main pipe can simplify reinforcement calculations or reduce the need for added pads, although this should be weighed against higher welding heat input and fabrication effort.
Thin-wall stainless steel pipe also demands more discipline during fabrication. Heat input control, distortion, root alignment, purge quality, and the risk of burn-through become more sensitive as wall decreases. If shop capability or field conditions are not ideal, an extremely light wall may create avoidable rework. The correct engineering choice is not always the thinnest code-compliant schedule if fabrication reliability is poor at that thickness.
Pressure is only one load case
Lines under pressure still see dead weight, fluid weight, insulation weight, occasional vibration, thermal displacement, and forces from connected equipment. Vacuum service can also matter if the system is steam cleaned or drained while hot. A wall chosen solely from internal pressure may be too flexible, may require closer support spacing, or may transmit unacceptable loads into pumps, vessels, or skids.
Where the line is subject to frequent thermal cycling, fatigue should be considered before reducing wall too aggressively. A thinner wall can lower thermal stress in some situations because it is more flexible, but repeated movement at branch points, restraints, and weld toes may still control the life of the line. The answer depends on the layout, support philosophy, and operating pattern, not on pressure rating alone.
Schedule 10S is not a universal economy option
In many stainless systems, Schedule 10S is attractive because it cuts weight and welding time. It can be a sound choice in clean, moderate-pressure service with suitable corrosion resistance and proper support design. The problem starts when that schedule is copied into lines with threaded components, severe cyclic conditions, uncertain corrosion, or frequent mechanical abuse during maintenance. Threads remove wall and can make thin schedules unsuitable. Grooving, repeated clamp loads, and aggressive line modifications during shutdowns can produce similar issues.
At the other extreme, jumping directly to Schedule 80S for comfort can waste material, increase hanger loads, complicate forming and welding, and create procurement mismatches when valves and fittings were specified around a lighter schedule. Thickness should solve a defined engineering need. If there is no such need, extra wall simply adds cost and weight to the steel package and to every downstream activity that handles it.
Material grade and wall thickness interact
The choice between common stainless grades may influence thickness indirectly through allowable stress, corrosion performance, and fabrication practice. A more corrosion-resistant grade does not automatically allow a thinner wall under pressure, but it may justify a smaller corrosion allowance where service conditions are well understood. Conversely, selecting a lower alloy grade for cost reasons can force a thicker wall or tighter inspection regime if corrosion uncertainty remains.
Surface finish and supply form also deserve attention. Seamless and welded pipe may follow different availability patterns depending on size and schedule. Lead time can become a practical constraint when the calculated requirement falls between common stocked thicknesses. In that situation, the realistic options are often to move up one schedule, revise the material grade, or revisit the design basis if an overly conservative input has been carried through the calculation.
Where selection mistakes usually begin
Several errors appear repeatedly in pressure piping work. One is using the operating pressure instead of the design pressure from the line class or datasheet. Another is forgetting to include mill tolerance before comparing required thickness with a nominal schedule. A third is borrowing a corrosion allowance from carbon steel service and applying it without reviewing whether the stainless corrosion mechanism is actually uniform wall loss. Equally risky is the opposite mistake: assigning no allowance because the word stainless appears in the material description.
There is also a coordination issue between process, piping, mechanical, and construction teams. If one discipline assumes butt-welded joints and another later inserts threaded instrument takeoffs or mechanical couplings, the original wall decision may no longer hold. The same can happen when support spacing, insulation density, or cleaning chemistry changes after the pipe class is issued.
A practical path to selection
The cleanest approach is to establish the controlling design condition, calculate the required minimum wall under the applicable code, add any corrosion or erosion allowance justified by service, account for manufacturing tolerance if the code basis requires it, and then choose the next available schedule that leaves reasonable margin for fabrication and operation. After that, review the fittings, branch details, support loads, and installation method against the selected wall. If any of those items become difficult, revisit the schedule before procurement rather than forcing the issue in the field.
- Where pressure is high relative to diameter, the pressure formula will often drive the result directly and the next heavier standard schedule may be the obvious answer.
- On large-diameter lines at moderate pressure, stiffness, vacuum risk, and handling damage may govern even when the pressure requirement alone suggests a very light wall.
- For corrosive or uncertain service, wall selection should be reviewed together with grade selection, because adding thickness to an unsuitable alloy can delay failure without removing the cause.
- If the selected wall pushes fabrication into a difficult range for purge welding, branch fit-up, or field alignment, a modest increase in thickness can reduce project disruption more effectively than repeated repair work.
Procurement and installation effects are real
Thickness affects more than pressure capacity. Heavier wall increases bundle weight, lifting requirements, spool support during transport, and fit-up effort at site. Lighter wall can lower handling loads but may demand better end protection, more careful storage, and tighter control of clamp points to avoid denting. These are not secondary details when the line includes long shop-fabricated spools or remote installation conditions.
Specification language should also be consistent across pipe, fittings, flanges, and valves. A wall change made late in design can expose mismatched bore, incompatible branch assumptions, or missing fitting schedules. Stainless steel pipe packages tend to become expensive when corrections happen after release because replacement pieces are often smaller in quantity and less likely to align with stock availability.
The right wall thickness is the one that remains adequate after pressure, temperature, corrosion, tolerance, fabrication, and service loads are all considered together. If a chosen schedule only works when every assumption stays ideal, it is too thin for a real project environment. If it adds weight without solving any identified risk, it is too thick.
Please give us a message
Tianjin Kaichuang Metal Material Co., Ltd
Add: No. 41, District 6, First Street, Huanghuadian Town, Wuqing District, Tianjin
Tel: + 86 137 9101 9833
E-mail: boss@kaichsteel.com