Steel Hub
How to Verify Steel Inspection Requirements Before Project Delivery
Before steel leaves a mill, stockholder, fabricator, or supplier warehouse, the question is not simply whether the material looks acceptable. Project leaders need to establish whether the delivered steel can be proven to meet the purchase order, design specification, applicable code, and intended service conditions. That proof may involve chemical composition, mechanical properties, dimensions, surface condition, traceability, testing records, and release documentation.
A weak steel inspection process often becomes visible only after delivery: a plate cannot be traced to its certificate, a structural section falls outside the agreed tolerance, pipe test records do not match the supplied heat numbers, or a coating requirement was assumed rather than written into the order. At that point, replacing material can affect fabrication sequences, transport planning, site installation, and the schedules of multiple subcontractors.
Steel is an upstream material with consequences throughout the supply chain. Produced from iron ore and scrap through ironmaking, steelmaking, and rolling, it reaches projects in forms as different as plate, beams, channels, hollow sections, pipe, wire rod, and reinforcing products. Construction, shipbuilding, energy, rail, automotive, and equipment projects do not use these products in the same way. Inspection requirements therefore cannot be copied unchanged from one order to the next.
Start with the requirement hierarchy, not the inspection checklist
The most reliable inspection starts before a purchase order is released. Build a clear hierarchy of requirements and resolve conflicts early. In many projects, the contract or technical specification takes priority, followed by approved drawings, referenced product standards, purchaser specifications, and supplier procedures. The exact order should be stated in the contract documentation; it should not be left to interpretation during final inspection.
This matters because a material grade alone is rarely a complete requirement. A designation may identify a family of steel, but the project may also require a particular delivery condition, impact-test temperature, thickness range, through-thickness performance, ultrasonic examination level, dimensional tolerance class, welding-related restriction, or corrosion-protection system. A buyer who writes only a grade and quantity may receive technically legitimate material that is still unsuitable for the project.
Review the order line by line and convert it into inspection points. For each product, define the required standard, grade, size, length or weight basis, delivery condition, test obligations, certificate type, marking method, packaging, and acceptance authority. If the project references standards such as ASTM, EN, ISO, API, or a national construction code, confirm the edition named in the contract. Substituting a newer or “equivalent” edition without formal approval can create a documentation problem even where the material appears technically comparable.
Translate the specification into a practical inspection and test plan
An inspection and test plan, often called an ITP, makes responsibilities visible. It should identify what is checked, when it is checked, which records are generated, and whether the purchaser or third-party inspector has a hold point, witness point, review point, or no attendance requirement. The purpose is not to add paperwork; it is to avoid discovering a critical requirement after the relevant production stage has passed.
For mill-produced material, key stages may include charge or heat identification, chemical analysis, rolling, heat treatment where applicable, mechanical testing, dimensional inspection, non-destructive testing, marking, and final loading. For fabricated structural steel, additional stages may include cutting, fit-up, welding procedure control, weld inspection, surface preparation, coating application, and trial assembly where specified.
The inspection plan should also state the sampling basis. This is especially important where an order contains several heats, thicknesses, or production lots. A test result from one heat cannot automatically validate another. Likewise, one dimensional check on a bundle does not prove conformity across a mixed shipment. The applicable product standard may define test units and sampling frequency, but the project specification may impose additional controls.
Check certificates for traceability, not just for presence
Material test certificates are central to steel inspection, yet they are often reviewed too late or too superficially. A certificate should be read as a traceability document, not treated as a generic quality attachment. Verify that the producer name, certificate reference, heat or cast number, product description, dimensions, grade, standard, delivery condition, and reported test results correspond to the actual goods and the order requirements.
For projects that specify EN 10204 inspection documents, the required document type should be agreed before production and clearly shown in the purchase order. The practical distinction is significant: some documents are based on non-specific inspection, while others report results from specific inspection and may involve validation by an authorized inspection representative. The correct type depends on the contract and project risk, not on a general preference for more documentation.
Traceability must survive handling. Heat numbers can be lost when plates are cut, bundles are split, sections are blast-cleaned, or material is transferred between warehouses. Ask how identification will be maintained through these stages. Acceptable methods may include durable stamping where permitted, tagged bundles, controlled transfer records, or a documented traceability map. If material is supplied as cut lengths or fabricated parts, the connection back to the original mill certificate needs to remain auditable.
A common warning sign is a certificate that matches the grade but not the size, heat number, or quantity delivered. Another is a certificate issued for parent material when the order actually includes fabricated, coated, or welded components with separate inspection requirements. Do not assume the mill certificate closes the entire quality file.
Match inspection methods to the product and service risk
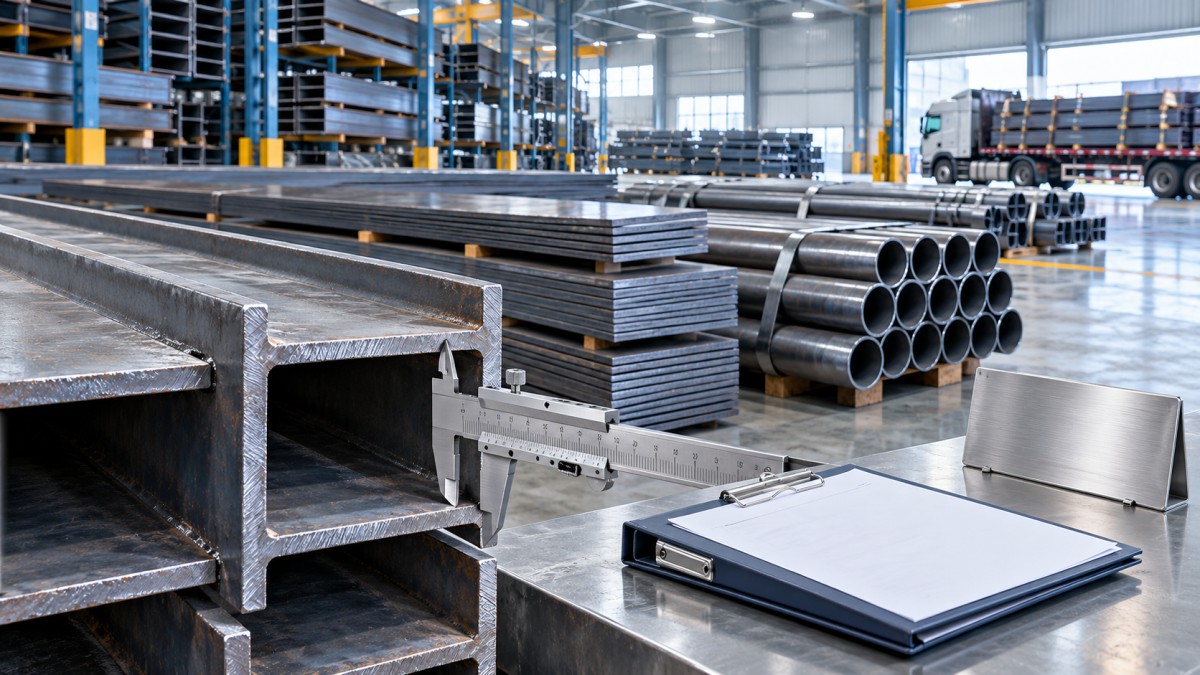
Not every steel product needs the same level of examination. Structural sections may require careful dimensional checks, visual examination for handling damage, and confirmation of straightness, twist, flange thickness, and profile tolerance. Plate used in highly restrained welded structures may need additional attention to laminar imperfections, thickness tolerance, edge condition, and properties relevant to the fabrication process. Pipe and tube projects may require checks for outside diameter, wall thickness, ovality, end preparation, test pressure records, or specified non-destructive examination.
The relevant standard should determine baseline acceptance criteria. Where the design or service conditions justify it, the purchaser may specify supplementary testing. Ultrasonic testing can be relevant for plate or forged products where internal discontinuities matter. Positive material identification may be useful when alloy mix-up is a credible risk. Charpy impact testing is not a decorative line item; its temperature, orientation, specimen location, and acceptance values must align with the requirement being invoked.
Avoid requesting tests without defining the method and acceptance basis. “NDT required” is incomplete. The order should identify the examination method, coverage, applicable procedure or standard, qualification expectations where relevant, reporting format, and acceptance level. The same applies to coating inspection. If steel is to be blasted and painted, clarify the specified surface-preparation grade, coating system, dry film thickness requirements, repair procedure, and inspection records expected before dispatch.
Control dimensional tolerance and usable condition
Material can meet its chemistry and tensile requirements yet still disrupt fabrication. A plate outside the agreed thickness tolerance may affect design calculations or fit-up. Excessive camber in a section can increase corrective work. Pipe end damage may delay welding preparation. For long products, bundle condition, straightness, coil integrity, and actual length can affect automated processing and site handling.
Use the tolerance standard stated in the order, and distinguish between nominal size and permissible variation. If tighter-than-standard tolerances are necessary, they should be written explicitly and accepted by the supplier before manufacturing. This is particularly important for components intended for robotic welding, modular construction, precision machining, or connection details with limited adjustment capacity.
Visual inspection should also address practical usability: corrosion, dents, gouges, edge damage, rolling defects, moisture exposure, contamination, and packaging failures. Minor surface conditions may be acceptable under the governing standard, but their acceptability can change when the material will receive a high-performance coating, be cold formed, or remain exposed in a demanding environment. Record any concession decision rather than relying on verbal acceptance at the loading point.
Define release authority and manage nonconformities before shipment
Inspection has limited value if no one knows who can release the material. The ITP and purchase documents should identify whether release is made by the supplier’s quality function, the purchaser’s representative, an independent inspector, or more than one party. A hold point means work should not proceed without the defined release; a witness point generally permits the supplier to continue if proper notice has been provided and attendance does not occur. The meaning should be agreed, not assumed.
When a deviation appears, separate it from a routine observation. A nonconformance should identify the affected material, requirement, actual condition, proposed disposition, and traceability impact. Possible outcomes may include replacement, rework where technically permissible, use-as-is through a formal concession, or rejection. Project teams should be cautious with informal statements such as “acceptable for the application.” Only the party with engineering and contractual authority should approve a departure from the requirement.
Shipment should not be released until the documentation package is complete enough for receiving inspection. Depending on the order, that package may include certificates, inspection reports, NDT reports, coating records, packing list, weight list, photographs, release note, and a nonconformance register showing closure status. Check that document revision numbers and material quantities align with the final shipment, especially after partial deliveries or substitutions.
Use a final pre-delivery review that reflects site reality
The final review is where technical compliance meets delivery control. Confirm that each bundle, plate, pipe length, or fabricated assembly is identifiable; that quantities and weights reconcile with the packing list; that loading will not damage finished surfaces; and that unloading constraints are understood. Long structural members, coated pipe, and precision-cut items may need particular lifting, separation, or weather-protection measures.
It is also worth asking a simple question: can the receiving team verify the shipment without searching through several unrelated files? If certificate references, package numbers, and material markings cannot be connected quickly, the project has inherited avoidable risk. A clear delivery dossier makes quarantine, installation release, and later audit much easier.
Good steel inspection is not a final gate imposed on a supplier. It is a controlled chain from specification through production, testing, documentation, loading, and receipt. For project delivery, the most useful discipline is to define the evidence required before the steel is made, preserve traceability while it is handled, and resolve every exception before the material becomes a site problem.
Please give us a message
Tianjin Kaichuang Metal Material Co., Ltd
Add: No. 41, District 6, First Street, Huanghuadian Town, Wuqing District, Tianjin
Tel: + 86 137 9101 9833
E-mail: boss@kaichsteel.com